Explore our flagship engineered fabrics tailored for international commercial, fashion, and industrial applications.
A comprehensive technical analysis of single-knit and double-knit cotton jersey architectures, CE regulatory compliance, and mechanical performance parameters.
CE certification for textile fabrics guarantees that every square meter of cotton jersey meets stringent European Union safety, health, and environmental criteria. Beyond physical safety, CE marking verifies strict adherence to REACH regulations regarding non-toxic azo dyes, heavy metal thresholds, and zero formaldehyde discharge.
Utilizing high-gauge circular knitting equipment (up to 36G), our 100% combed cotton jersey achieves exceptional natural 4-way mechanical stretch without requiring synthetic elastane, preserving pure tactile comfort, high breathability, and structural recovery.
Integrating CE standards with OEKO-TEX Standard 100 (Class I for infant safety) and GOTS (Global Organic Textile Standard) ensures complete traceability from organic long-staple raw cotton sourcing to bio-enzymatic finishing processes.
| Fabric Parameter | Standard Single Jersey | Interlock Double Jersey | Mercerized Cotton Jersey | Testing Protocol |
|---|---|---|---|---|
| GSM Range (g/m²) | 140 GSM - 220 GSM | 200 GSM - 320 GSM | 160 GSM - 240 GSM | ISO 3801 / ASTM D3776 |
| Yarn Count Options | 30s/1, 40s/1 Combed | 40s/2, 50s/2 Compact | 60s/2, 80s/2 Gas-Singed | ISO 2060 |
| Dimensional Shrinkage | < 3.0% (Post Compactor) | < 2.0% (Heat Set) | < 1.5% (Pre-Shrunk) | ISO 6330 / AATCC 135 |
| Color Fastness (Washing) | Grade 4-5 | Grade 4-5 | Grade 5.0 | ISO 105-C06 |
| Pilling Resistance | Grade 4 (Martindale) | Grade 4-5 | Grade 5.0 | ISO 12945-2 |
| CE Certification Status | Fully Compliant (EU Directives) | Fully Compliant (EU Directives) | Fully Compliant (EU Directives) | EN ISO 13688 Alignment |
Combining modern industrial knitting technologies with strict custom OEM frameworks to empower global buyers across fashion, home textiles, and technical industries.
Shenzhen Harbor Textiles Co., Ltd. is a leading luxury textile fabric manufacturer based in Shenzhen, China, specializing in high-quality fabrics for fashion, home décor, and toy applications. With extensive experience in the textile industry, Harbor Textiles has earned a reputation for producing premium faux fur, fleece, plush, and toy fabrics, offering both innovation and craftsmanship to meet diverse client needs.
By blending state-of-the-art circular knitting machines with rigid micro-defect scanning systems, Harbor Textiles seamlessly bridges the gap between massive scale production and fine bespoke fabric design.
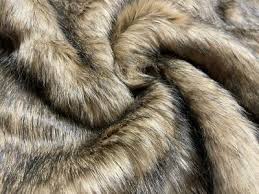
The company focuses on custom OEM services, providing tailored solutions for international buyers, including fashion brands, home textile retailers, and toy manufacturers. By combining advanced machinery, professional design teams, and strict quality control, Harbor Textiles ensures each fabric delivers softness, durability, and aesthetic appeal, meeting both functional and decorative requirements.
Harbor Textiles emphasizes sustainable and eco-friendly production, sourcing materials responsibly and adopting environmentally conscious manufacturing practices. Its design team continuously develops trend-driven fabric collections, including seasonal patterns, unique textures, and specialty finishes, helping clients stay ahead in competitive markets.
As a trusted partner in the textile industry, Shenzhen Harbor Textiles Co., Ltd. provides end-to-end solutions, from fabric concept and design to production, finishing, and packaging. Whether supplying luxury faux fur for fashion, fleece for home textiles, or soft fabrics for plush toys, Harbor Textiles remains committed to quality, innovation, and customer satisfaction, making it a preferred choice for brands and manufacturers seeking reliable and premium textile solutions from China.
Unmatched raw material sourcing, automated processing ecosystems, and rapid export capabilities from the Greater Bay Area.
Direct integration with certified long-staple cotton farms allows us to secure raw fiber length exceeding 38mm. This yields cotton yarn with higher tensile strength, reduced nep count, and superior luster after knitting.
Situated in Shenzhen's technological hub, Harbor Textiles leverages Yantian and Shekou deep-water ports. Containerized fabric shipments reach major European and North American ports up to 7 days faster than inland nodes.
Our facility incorporates automated fabric scanners with AI image recognition to pinpoint weaving flaws, color shade variations, or drop stitches in real time, assuring a zero-defect standard for export rolls.
Standardized international purchasing procedures designed for high-volume textile brands, OEMs, and retail fashion conglomerates.
Every custom color request undergoes Datacolor spectral analysis. We issue standard 4-option lab dips (A, B, C, D) within 72 hours, ensuring precise color temperature and illuminant match (D65, TL84, CWF) prior to bulk dye-lot authorization.
Following ASTM D5430 guidelines, all produced cotton jersey fabric rolls undergo rigorous 4-Point System evaluation. Defect penalty points per 100 square yards are maintained below strict international brand thresholds (< 20 points).
Pioneering functional treatments, bio-based fiber blends, and smart textile technologies for modern apparel markets.
Incorporating micro-encapsulated phase change materials (PCM) directly into the jersey knit matrix, allowing garments to absorb body heat during active exertion and release thermal energy during rest phases.
Transitioning to closed-loop supercritical carbon dioxide fluid dyeing eliminates wastewater discharge, reducing energy consumption by 40% while achieving ultra-vibrant, deep color saturation in cotton jersey fabrics.
Permanently bonded silver nanoparticles prevent bacterial proliferation on cotton jersey surfaces, providing long-lasting odor resistance for activewear, underwear, and medical apparel applications across 50+ wash cycles.
Tailored performance specifications meeting regional regulatory demands and consumer expectations across diverse market segments.
Our high-gauge mercerized cotton jersey provides a silky drape, subtle luster, and exceptional skin-touch comfort, making it the preferred choice for high-end T-shirts, loungewear, and premium casual fashion in Europe and North America.
Engineered without harsh softeners or optical brighteners, our CE and OEKO-TEX certified Class I babywear fabrics ensure zero skin irritation, maximum breathability, and non-allergenic safety for delicate baby skin.
Interlock and fleece jersey fabrics are optimized for structural elasticity and dimensional stability, serving as resilient backings and linings for furniture upholstery, decorative pillows, and indoor curtains.
In addition to jersey knits, Harbor Textiles delivers custom plush, fleece, and weather-resistant synthetic materials designed to withstand mechanical strain and environmental exposure for soft toys and technical gear.
Direct answers to technical, regulatory, and procurement inquiries regarding CE certified cotton jersey fabric production.
Discover our extended line of high-durability, eco-friendly, and decorative fabrics engineered for global markets.
 Harbor Textiles